In brief:
• Belt conveyor maintenance centers on tracking, tension, guarding, and lockout/tagout checks performed on a consistent schedule.
• CEMA and OSHA guidelines shape most industrial maintenance routines, including those manufacturers follow.
• Choosing between in-house upkeep and manufacturer-supported service depends on facility size, parts availability, and downtime tolerance.
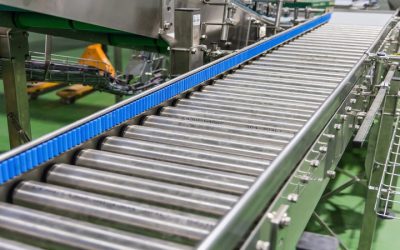
Belt conveyor maintenance keeps bulk material handling systems running safely and efficiently by catching wear, misalignment, and component failure before they cause downtime. For facilities, the right maintenance approach depends on production volume, material type, and how quickly replacement parts can be sourced.
Industrial operators researching belt conveyors often start with a basic question: should maintenance be handled internally or coordinated with the equipment manufacturer? Both paths work, but they carry different trade-offs in cost, response time, and long-term reliability. Understanding what each option involves helps plant managers set realistic maintenance schedules before equipment problems force a decision.
What Belt Conveyor Maintenance Actually Involves
Maintenance routines are typically organized by component rather than by calendar date, since different parts wear at different rates. A structured approach groups inspection tasks into a handful of recurring zones:
• Belt surface and tracking – checking for cuts, slippage, carryback, and alignment across idler stations.
• Drive system – monitoring motor temperature, amperage, gearbox condition, and belt tension.
• Transfer points – inspecting skirtboard seals and chutes for wear or blockage.
• Safety devices – testing pull cords, drift switches, and nip-point guards.
This component-based method is recommended because it structures conveyor checklists around what is being inspected rather than when, which makes routes faster, training simpler, and findings easier to trend over time. Facilities that skip this structure often find problems only after a failure has already caused unplanned downtime.
Regulatory Guidelines That Shape Maintenance Schedules
Maintenance timing is not arbitrary. Federal safety standards set minimum expectations for how often conveyors should be inspected and how maintenance work must be performed.
OSHA’s general industry rules require clear control of hazardous energy, meaning lockout and tagout procedures must be followed before cleaning, adjusting, or repairing conveyor systems. Guarding requirements are equally specific: guards must be securely attached, and OSHA regulations require them to be removable only with tools. For a fuller breakdown of federal conveyor safety expectations, the Mine Safety and Health Administration’s conveyor systems guidance outlines practices relevant beyond mining settings, including lockout procedures and guarding near moving parts.
Beyond regulatory minimums, industry-specific engineering standards add another layer of guidance. Conveyor systems also follow industry-specific standards set by the Conveyor Equipment Manufacturers Association, which provides standardized technical guidelines and best practices. These CEMA standards influence belt sag tolerances, component sizing, and splice specifications that maintenance teams reference during inspections.
In-House Maintenance vs. Manufacturer-Supported Service
Operations weighing how to structure upkeep generally choose between building an internal maintenance program or relying on a manufacturer’s parts and engineering support. The table below compares common trade-offs.
| Factor | In-House Maintenance | Manufacturer-Supported Service |
| Parts sourcing | Depends on stocked inventory and local suppliers | Often tied to manufacturer stock and shipping timelines |
| Technical expertise | Relies on internal training and documentation | Benefits from engineering familiarity with original specs |
| Response time | Immediate if staff and parts are on hand | Dependent on manufacturer turnaround commitments |
| Long-term cost | Lower per-task cost, higher risk of unplanned downtime | Potentially higher per-service cost, more predictable uptime |
Neither path eliminates the need for routine inspection. OSHA requires employers to establish maintenance schedules, document inspections, and take immediate corrective action when issues are detected, regardless of who performs the work.
Frequently Asked Questions
How often should belt conveyors be inspected? Inspection frequency depends on duty cycle and material abrasiveness, but safety devices such as pull cords and guards are commonly checked weekly as part of routine rounds.
What is the biggest safety risk during conveyor maintenance? Failing to de-energize equipment before servicing is a leading cause of incidents. Lockout/tagout includes de-energizing equipment and securing controls to prevent accidental restart, and failure to follow these procedures commonly causes conveyor-related injuries.
Do all conveyor guards need to meet the same standard? Guard specifications vary by opening size and proximity to moving parts. ANSI standards provide detailed guidelines specifying that larger openings in a guard require greater separation distance from rotating equipment.
Can maintenance needs differ between industries? Yes. OSHA’s general industry standards cover guarding, lockout/tagout, and emergency stop requirements for most manufacturing facilities. At the same time, mining operations fall under stricter MSHA rules, and FDA regulations require sanitary design for contamination-sensitive environments.
A Practical Next Step for Facilities
Reliable conveyor performance depends on consistent inspection habits, clear documentation, and access to parts when components wear out. Orthman Conveying Systems designs and manufactures custom bulk material handling equipment, including conveying systems built to CEMA standards, from its facility. Facilities evaluating maintenance plans or sourcing replacement components can review engineering specifications and request a quote directly to align equipment upkeep with operational schedules.